COMPLETE EXTRUSION. ENGINEERED AS ONE.
Downstream

Protect profile quality from the press exit to finished length.

Downstream equipment must guide hot profiles through rapid cooling, controlled transfer, stretching, cutting and inspection without introducing avoidable distortion or surface damage. ALUFORMIX develops each downstream stage around the profile mix, alloy requirements, press output and plant-handling method.

Equipment

ALUFORMIX Downstream equipment

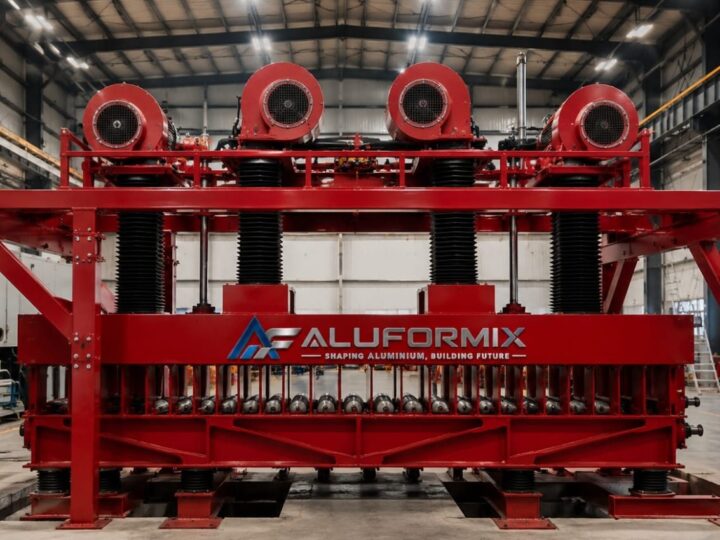
ALUFORMIX intensive air quench system at the press exit of an aluminium extrusion line

Quenching System

Cools the profile immediately after extrusion using air, water mist, spray or a combined system selected according to alloy, profile geometry and required metallurgical response. Zoning and flow control can be configured to support different production recipes.

  • Air, water or combined cooling concepts
  • Upper, lower and side-zone arrangements
  • Adjustable flow and recipe parameters
  • Drainage, extraction and enclosure by project design
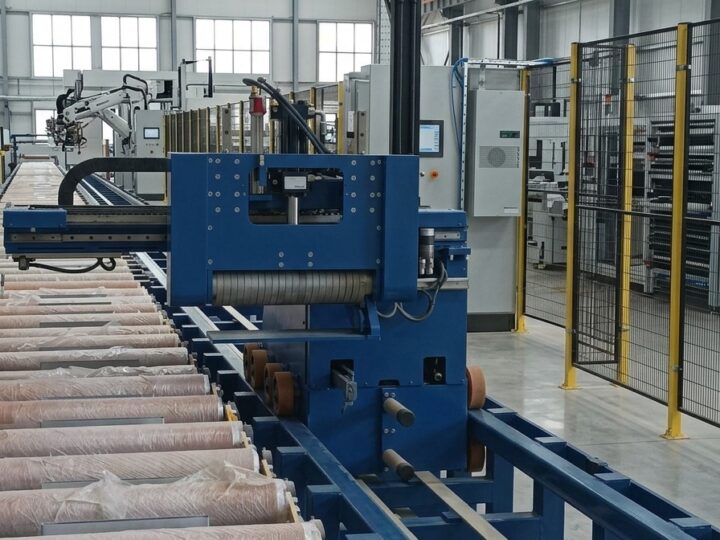
ALUFORMIX lead out tables with puller railway track for aluminium profile extraction

Lead-Out Table

Supports the profile directly after the press and quench zone, maintaining a stable path into the puller and cooling-table sequence. Contact materials and support arrangement are selected for temperature and surface protection.

  • Temperature-resistant rollers or belts
  • Alignment with press exit
  • Service access around the quench area
  • Integration with puller travel
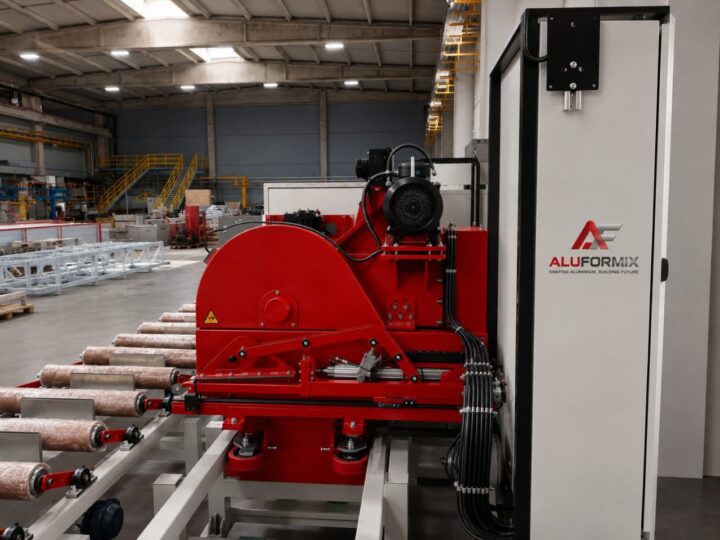
ALUFORMIX puller with integrated puller saw on the extrusion run-out

Pullers & Puller Saw

Guides the emerging profile through the run-out area and coordinates separation at the required point. Configurations can include a single puller, dual pullers and positioned or flying-saw arrangements.

  • Single- or dual-puller concepts
  • Synchronized motion with press speed
  • Controlled gripping for profile protection
  • Automatic cut and cycle sequencing
Automatic Puller System →Flying Saw →
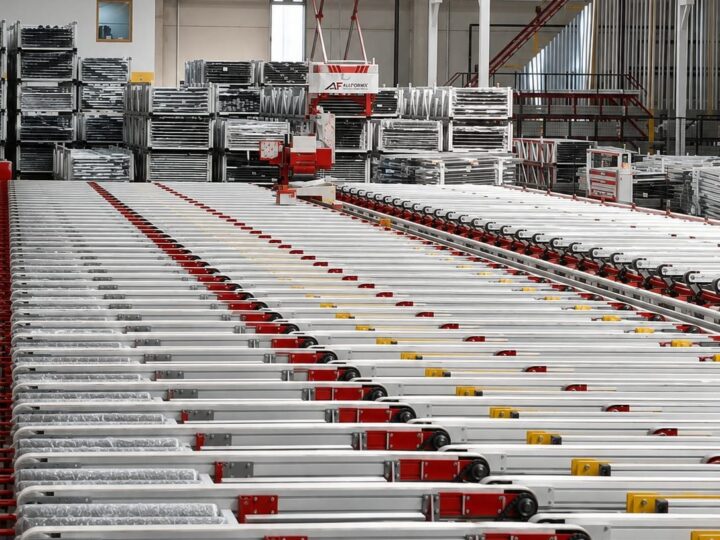
ALUFORMIX cooling and handling tables carrying extruded aluminium profiles

Cooling Tables

Support profiles while heat is removed before stretching. Table length, transfer method, fan arrangement and accumulation strategy are configured around the profile range and required cooling time.

  • Belt, roller or walking-beam transfer options
  • Axial-fan and ducted cooling arrangements
  • Sectional movement and buffering
  • Surface-protection materials by application
Cooling Table →
ALUFORMIX cooling and handling tables carrying extruded aluminium profiles

Cooling & Handling Tables

Move profiles between cooling, stretching, cutting and inspection areas while maintaining organized batches. The handling concept is selected to reduce unnecessary contact and preserve line flow.

  • Cross-transfer and longitudinal movement
  • Batch separation and accumulation
  • Automatic or operator-assisted modes
  • Integration with stretchers and saws
ALUFORMIX cooling and handling tables carrying extruded aluminium profiles

Stretcher with Stretcher Beam

Applies controlled tensile deformation to straighten profiles and relieve process-induced distortion. Clamping force, beam structure, stroke and control are selected according to profile dimensions and mechanical requirements.

  • Single- or double-head movement concepts
  • Configurable clamping arrangement
  • Recipe and stretch-length control
  • Guarded operating zone and safe access
Stretcher Machine →
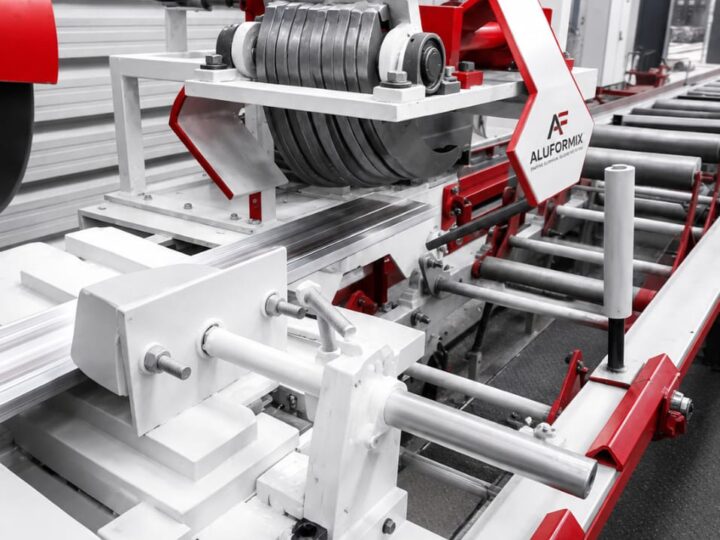
ALUFORMIX profile flying cut saw and clamping section on the extrusion line

Profile / Cold Saw

Cuts cooled and stretched profiles to the required finished length. The saw system is designed around length tolerance, bundle or layer handling, profile dimensions and chip-control needs.

  • Length-stop or servo-positioning options
  • Single-profile, layer or batch-cutting concepts
  • Chip and dust extraction interface
  • Loading and unloading tables
ALUFORMIX cooling and handling tables carrying extruded aluminium profiles

Inspection Table

Presents cut profiles for visual, dimensional or sample-based inspection before stacking and ageing. The layout can support manual quality checks, measuring tools and controlled transfer to the next stage.

  • Accessible inspection position
  • Lighting and measurement provisions
  • Reject or rework routing
  • Integration with stacking sequence

Engineer a complete downstream solution

Send your profile range, press size, run-out length, alloy mix, quench requirement and available floor space for a downstream concept discussion.

Call WhatsApp Enquire